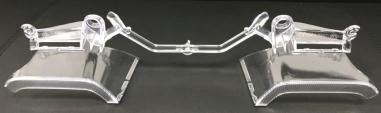
Injection-molded transparent and complex appearance parts. The part shown is a representative example — a mirrored pair of clear parts combining solid block sections with slender cantilever beams and upward-curving arms, including circular ring or boss features and multiple complex curved transitions. Custom tooling, material selection and integrated finishing available.
Custom Transparent & Complex Appearance Parts | Clear Injection Molding
| Recommended Resins | PC, ABS, PC+ABS, PA66+GF, POM, PBT, PMMA, TPU, PEEK (RoHS / REACH) |
|---|---|
| Tooling & Molding | Precision Multi-Cavity Tooling, Cold/Hot Runner, High-Gloss Molding, 2K Insert Overmolding |
| Tooling Precision | ±0.01 mm (High-speed CNC, Mirror Spark EDM, Slow Wire Cutting) |
| Secondary Finish | SPI A2 Mirror Polish, VDI / MT Texture Grain, Silk-Screen Printing, Vacuum Metalizing |
| T1 Sample Lead Time | 15 – 25 Working Days (DFM Analysis delivered within 24 Hours) |
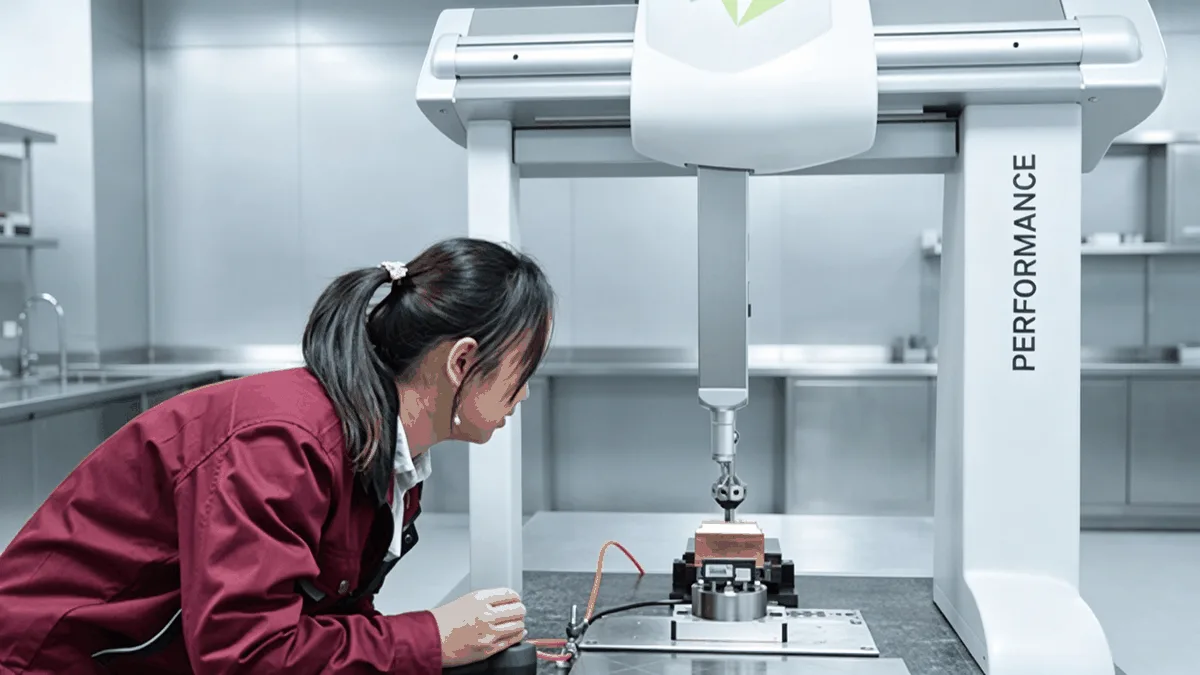
| Quality Assurance | 100% CMM Dimension Verification, Color Spectrophotometer, FAI Report |
Part Details & Engineering Gallery
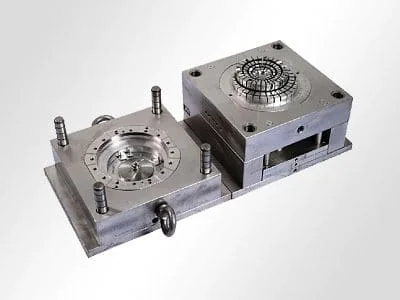
Close-up views of mold fitting, surface finish, and precision structure.
Capability & Engineering Review
What it is
Transparent and complex appearance parts serve applications with requirements on optical behaviour, curvature complexity and appearance consistency. Compared with opaque structural parts, these parts carry an extra constraint: internal defects have nowhere to hide once the part is transparent — sink marks, weld lines, flow marks, black spots and internal stress may be invisible on an opaque part but show up directly as visible optical defects on a clear one.
The manufacturing challenge here is not whether the part can be made, but whether conforming parts with consistent appearance can be produced reliably.
Structural features visible in the product photo
The part shown is a mirrored pair of high-clarity injection-molded parts. Each consists of three sections: a solid block at the outer end with an angled underside; a slender cantilever beam extending inward from the block; and an upward-curving arm at the beam’s end, terminating in a circular ring or boss feature. A horizontal rail connects the two parts, with a small protrusion beneath the centre of that rail.
Light passing through the parts shows clear refraction and bright edges, indicating significant wall-thickness variation along the length.
Manufacturing capability
The part is developed on in-house tooling design and manufacturing. The toolroom runs wire EDM, jig grinding, surface grinding, form grinding, CNC machining centres and EDM, forming a complete precision machining chain. On the molding side, 20 in-house machines combine all-electric, servo and vertical presses, with coordinated 100–2000T trial and production resources.
Appearance surfaces on transparent tooling normally require mirror-grade polishing and high-polish mold steels — see Section H for the actual capability position.
Integrated finishing
After molding, spray coating, silk-screen printing, pad printing, electroplating and anodizing can be integrated. Transparent parts commonly also require high-gloss or UV coating, screened window areas and edge polishing or deflashing — reducing multi-supplier coordination and the quality handover risk it brings.